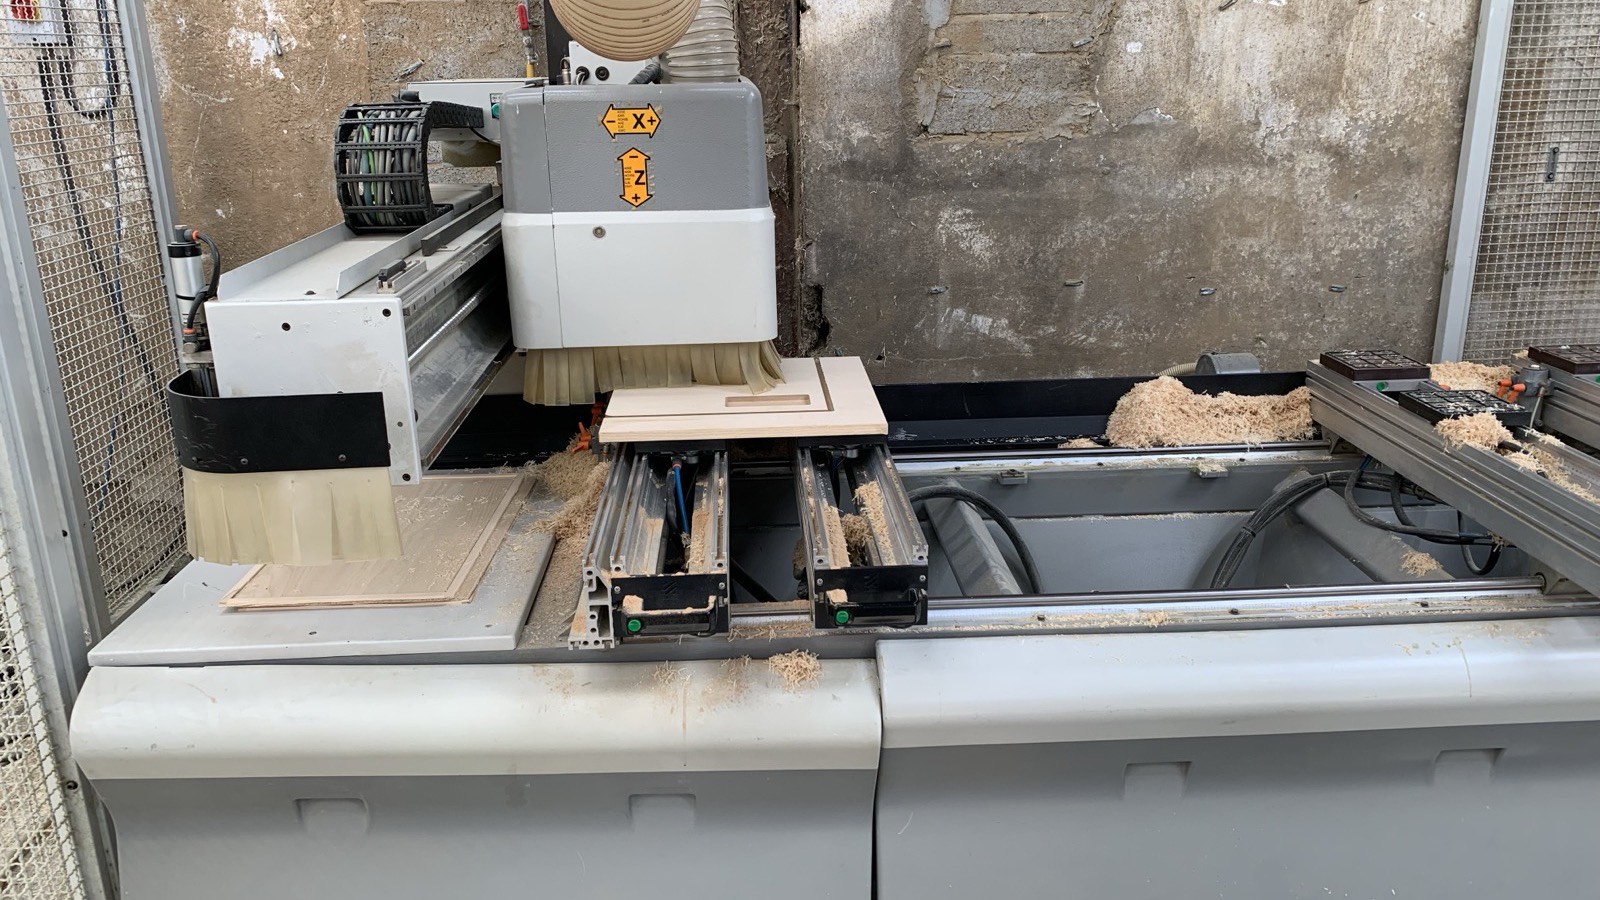
Yes, Autodesk Fusion can often be used successfully with older CNC machines. The age of the machine itself is usually less important than the capabilities of its CNC controller, supported program format and the quality of the post processor.
Older machines may have limited program memory, slower block processing, restricted support for arcs or special machine-specific programming formats. These limitations do not automatically mean that the machine needs a new controller or cannot be programmed from Fusion.
With the correct CAM settings and a properly configured post processor, many older woodworking and metalworking CNC machines can still be integrated into a modern Fusion workflow.
Quick Answer
Can Fusion work with an old CNC machine? Usually yes, provided the machine can accept externally generated programs and its controller functions can be represented correctly by a Fusion post processor.
Typical limitations of older CNC controllers include:
- limited NC program memory
- slow processing of short toolpath movements
- restricted G2/G3 arc support
- proprietary NC program formats
- limited network or DNC connectivity
- machine-specific drilling cycles and macros
- older controller syntax
- limited support for modern 3D toolpaths
The post processor and CAM strategy must therefore be adapted to the capabilities of the actual machine.
In this guide
- Can Older CNC Machines Run Programs from Autodesk Fusion?
- What Determines Fusion Compatibility?
- Common Problems with Older CNC Controllers
- How to Optimize Fusion for an Older CNC Machine
- Smoothing
- CAM Tolerance
- Splitting Large Programs
- DNC and Drip Feeding
- Custom Post Processors
- When Fusion May Not Be the Right Solution
- How to Check Your CNC Machine
- Frequently Asked Questions
Can Older CNC Machines Run Programs from Autodesk Fusion?
Fusion does not normally control the CNC machine directly. CAM toolpaths are created in Fusion and a post processor converts those toolpaths into the NC program format required by the machine and its controller.
This means that compatibility is not determined simply by the age of the CNC machine. A 20-year-old machine can sometimes be easier to integrate than a much newer machine using a poorly documented proprietary control system.
The important question is whether the functions required by the machine can be represented correctly in the output generated by the Fusion post processor. Understanding what a CNC post processor does is the starting point for evaluating any older machine.
What Determines Fusion Compatibility?
Before developing or modifying a Fusion post processor for an older CNC machine, several things need to be checked:
CNC controller
The controller determines which commands, cycles, interpolation methods and program structures are available.
Examples can include controller families such as Fanuc, Siemens, Heidenhain and Osai, as well as proprietary woodworking CNC systems.
Program format
Some machines use standard or modified G-code, while woodworking CNC machines may use manufacturer-specific formats or higher-level machining instructions.
Machine configuration
The post processor must reflect the actual machine configuration:
- number of axes
- rotary axis configuration
- spindle configuration
- drilling heads
- aggregates
- tool changer
- work offsets
- machine coordinate system
- available machining cycles
Controller limitations
Older controllers may have significantly less memory and processing power than modern CNC controls.
Existing documentation
A known working NC program, programming manual and machine documentation can greatly simplify the development and validation of a post processor.
Common Problems with Older CNC Controllers

Limited Program Memory
One of the most common limitations of older CNC controllers is the amount of memory available for NC programs.
Modern CAM systems can generate very large programs, particularly for 3D machining. A program containing thousands of short movements may exceed the memory available on an older control even though the actual machining operation is relatively simple.
This can often be improved by optimizing the toolpath, smoothing the NC output, adjusting CAM tolerance or splitting the program into smaller sections.
Slow Block Processing and Data Starving
An older controller may be able to load the NC program successfully but still struggle to process it fast enough during machining.
Modern 3D CAM toolpaths can contain thousands of very short linear movements. If the controller cannot process the commands quickly enough, the machine may repeatedly slow down or hesitate.
This is commonly referred to as data starving.
Typical symptoms include:
- machine movement that is not smooth
- feed rate significantly below the programmed value
- visible hesitation during 3D machining
- poor surface finish
- long machining times
Reducing unnecessary NC blocks can therefore improve not only file size but also actual machine performance.
Limited Arc Support
Older controllers do not always support circular interpolation in every plane or configuration.
A post processor may therefore need to determine when G2/G3 movements can safely be used and when the movement needs to be linearized.
This behavior must be configured for the actual controller rather than assumed globally.
Proprietary NC Formats
Not every older CNC machine uses conventional ISO G-code.
This is particularly common in the woodworking industry, where CNC manufacturers often use proprietary program formats, drilling cycles, macros or higher-level machining instructions.
In these cases, the task of the post processor is not simply to change G-code syntax. It may need to translate Fusion CAM operations into a completely different machine-specific programming structure.
How to Optimize Fusion for an Older CNC Machine
Several approaches can be used depending on the limitation of the machine.
The correct solution should be selected based on the controller rather than simply reducing the quality of the CAM toolpath.
Solution 1: Use Fusion Smoothing
Fusion’s Smoothing option can reduce unnecessary points in a toolpath and replace groups of short linear movements with longer movements and circular arcs where the geometry and CNC controller allow it.
This can significantly reduce the number of NC blocks that need to be stored and processed by the CNC controller.

However, smoothing must be configured together with machining tolerance and the capabilities of the target controller. It should not be assumed that every older CNC supports every type of G2/G3 movement.
Solution 2: Optimize CAM Tolerance
CAM tolerance has a direct impact on the amount of data generated by a toolpath.
A very tight tolerance can create a much larger number of toolpath points. This may be appropriate for some applications but unnecessarily demanding for an older CNC controller.
A larger tolerance can reduce the number of generated movements, but it also changes the maximum allowed deviation from the calculated toolpath.
The objective is therefore not simply to use the largest possible tolerance. The goal is to find a suitable balance between:
- required machining accuracy
- surface quality
- NC program size
- controller processing capability
Tolerance and smoothing should normally be evaluated together.
Solution 3: Split Large NC Programs
If the main limitation is controller memory, another solution is to divide a large machining program into smaller NC files or subprograms.
Depending on the controller, a custom post processor can sometimes automate this process.
Possible approaches include:
- multiple independent NC programs
- main program with subprograms
- operation-based program splitting
- size-based splitting
The implementation depends on how the CNC controller manages files and program execution.
Solution 4: Use DNC or Drip Feeding
Some older CNC controllers support DNC or drip feeding, allowing an NC program to be transferred progressively to the controller while the machine is running.
This can allow programs larger than the controller’s internal memory to be executed.
DNC capability depends entirely on the machine and controller configuration and may use serial communication, network communication or dedicated DNC software. Fusion itself should not be described as the DNC system.
Solution 5: Adapt the Post Processor to the Controller
The post processor is often the key component when connecting a modern CAM system to an older CNC machine.
A custom Fusion post processor can adapt the output to the specific limitations and requirements of the controller. Depending on the machine, this can include:
- controller-specific program syntax
- G2/G3 limitations
- tool change logic
- drilling cycles
- work offsets
- rotary axis output
- machine macros
- subprograms
- program splitting
- safe retract behavior
- feed rate handling
- machine-specific headers and program structure
A post processor cannot add functionality that the CNC controller physically does not support, but it can ensure that Fusion uses the available functions correctly.
Fusion post processor development is the practical process behind every solution described above — see how .cps files and Post Properties actually work.
Every machine on this list starts from the same evaluation: see the full list of supported CNC machines and post processors we develop and adapt.
| Problem | Typical symptom | Possible solution |
|---|---|---|
| Limited controller memory | NC file cannot be loaded | Smoothing, tolerance optimization, program splitting or DNC |
| Slow block processing | Machine hesitates during machining | Reduce unnecessary short movements and optimize smoothing |
| Unsupported G2/G3 arcs | Controller reports arc errors | Configure post processor arc output or linearization |
| Unsupported syntax | Program is rejected by the CNC | Controller-specific post processor |
| Proprietary CNC format | Standard G-code cannot be used | Machine-specific post processor |
| No network connection | Difficult program transfer | Serial transfer, DNC or existing machine transfer method |
| Special drilling cycles | Incorrect drilling behavior | Machine-specific post processor logic |
| Large 3D programs | Slow execution or memory problems | Smoothing, tolerance optimization and controller-specific output |
What Types of Older CNC Machines Can Be Integrated?
There is no universal age limit for using Autodesk Fusion with a CNC machine.
Fusion can potentially be integrated with both metalworking and woodworking CNC systems as long as the programming requirements of the machine can be determined.
Examples may include machines using:
- Fanuc controls
- Siemens controls
- Heidenhain controls
- Osai controls
- SCM / Xilog systems
- SCM Maestro systems
- Biesse CNC systems
- Homag / Weeke systems
- Holzher / NC HOPS systems
Important: inclusion in this list must not imply that every machine or every controller version is automatically supported. Each machine must be evaluated individually.
Example: SCM Maestro / Xilog
Older SCM machines running Maestro or Xilog can use a machine-specific Fusion post processor to generate structured XCS output instead of generic G-code.
See the SCM Maestro XCS postprocessor →Example: Holzher / NC HOPS
Holzher woodworking machines using the NC HOPS format require a post processor that understands the native Holzher program structure, not conventional G-code.
See the Holzher NC HOPS postprocessor →When Fusion May Not Be the Right Solution
Not every older CNC machine can or should be integrated with a modern CAM system.
A Fusion workflow may not be practical when:
- external NC programs cannot be loaded
- the controller uses an undocumented proprietary format
- essential machine functions cannot be controlled externally
- machine documentation is completely unavailable
- the required operation is not supported by the controller
- the machine configuration cannot be safely reproduced in the post processor
In these situations, a controller retrofit, manufacturer-specific CAM system or another integration method may be more appropriate.
How to Check Whether Your CNC Can Work with Fusion
Before developing a post processor, I normally check the machine and controller configuration first.
To evaluate an older CNC machine, the following information is useful:
- machine manufacturer
- exact machine model
- machine year
- CNC controller or software
- number and configuration of axes
- example of a known working NC program
- programming manual if available
- operations that need to be programmed from Fusion
Not sure if your CNC machine can work with Autodesk Fusion?
Send me the machine model, controller information and an example of a working NC program. I can first evaluate whether creating a Fusion post processor for the machine is technically feasible.
Check My CNC Compatibility →Replacing a working CNC machine or controller is not always necessary. In many cases, the first step should be to determine whether the existing machine can be integrated with Fusion using the correct CAM configuration and post processor.
Send me information about your CNC machine and I will evaluate the required postprocessor solution.
